Hey there, fellow gearheads and manufacturing pros! If you’re in the market (or just curious) about Roll To Roll (R2R) heat transfer machines, you’ve probably wondered, “Wait—what even makes a good substrate for this stuff?” As someone who’s been supplying these machines for over 8 years now, I’ve seen it all: folks who skip the basics, end up ruining hundreds of yards of material, and then shoot me a frantic, 2 a.m. email asking if their substrate’s garbage or if they need a new machine. Let’s cut the corporate jargon, get real, and break down exactly what substrates need to nail R2R heat transfer—no fancy textbooks required. Roll To Roll Heat Transfer Machine
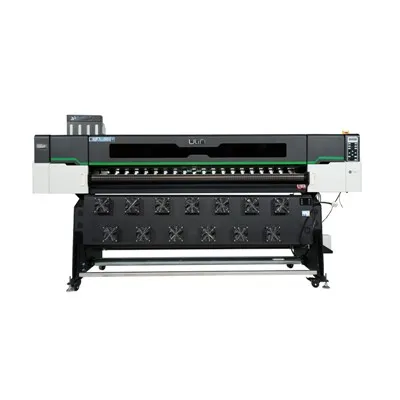
First off, let’s level-set: R2R heat transfer is all about continuous rolls of material, not just single pieces. That means it’s a total assembly line process—think 100-yard spools zipping through the machine at 10 to 50 feet per minute, depending on the job. Every inch has to be consistent, because if one spot on your spool is off, you’re tossing a whole roll. So substrates for this aren’t just “works with anything”—they have three core boxes to check: temperature tolerance, surface chemistry, and dimensional stability. Let’s dive into each, with real-world examples I’ve seen.
Temperature tolerance is non-negotiable, full stop. When your transfer film hits the substrate, it’s going from room temp to, well, hot—usually 250°F to 400°F, depending on the ink type. If your substrate can’t take that heat? You’re gonna get a mess. Not just blurry graphics, but maybe shrinkage, warping, or even melting in bad cases. Let’s talk about the two big substrate categories here, because that’s where most people mess up. For textile substrates—like polyester, nylon, or even cotton blends—you’ve got to check the fiber’s “glass transition temperature” (Tg, for short). Tg is the temp where the fiber’s molecular structure softens, so if you heat above that, it starts to deform. I had a customer last year who tried to use 100% cotton (Tg is way lower, like 200°F) with a transfer that needed 350°F. Halfway through the roll, the cotton started shrinking so bad the whole web got wavy, and the machine’s tension sensors (which are super precise) couldn’t keep up—total $1,200 roll loss. Compare that to polyester, which has a Tg around 150°F but can handle up to 420°F short bursts—perfect for most R2R jobs. For non-textile substrates, like vinyl, PET films, or even flexible packaging, same rule: check the heat resistance. If you’re working with, say, a cheap PVC vinyl that melts at 280°F, don’t use a transfer that needs 320°F. I always tell customers: pull up your substrate’s spec sheet first, before you even order transfer film. The sheet will have a “maximum processing temperature” line—stick below that, and you’re golden.
Next up, surface chemistry. This is the quiet culprit that ruins more transfers than heat tolerance, trust me. R2R heat transfer works because the ink or adhesive on the transfer film bonds to the substrate’s surface. If that surface is oily, dusty, has a chemical coating, or is just too smooth? The bond will be weak—you’ll get peeling, cracking, or even the whole graphic rubbing off after one wash. Let’s break this down. First, contamination: if your substrate came straight from the warehouse with a residue from manufacturing, like sizing on cotton or anti-static coating on plastic, that’s a no-go. I had a food packaging client last month who tried to use a PET film that had a factory anti-static spray—they couldn’t figure out why the labels kept peeling off until they wiped a test spot with isopropyl alcohol and it worked perfectly. So always pre-test for contamination: do a quick wipe with rubbing alcohol, let it dry, do a small test transfer. If it works? No residue. If not, you’ve got to degrease or clean the substrate first. Then there’s surface tension. Most transfer adhesives need a surface tension of 38 to 45 dynes/cm to bond well. If your substrate is too low (like untreated polypropylene, which is only 30 dynes/cm), the adhesive can’t “wet out” and stick. For smooth plastics, a quick corona treatment (a cheap, surface-level plasma blast) fixes this—we even include a free corona pre-treatment guide with every R2R machine we sell, because so many people forget that step. Textiles are a little easier here, but if you’re using a synthetic that’s been coated with a water-repellent or stain-resistant finish, that’s the same problem as contamination—you need to strip that coating first with a mild detergent or pre-treatment spray. I once had a customer who refused to pre-treat their polypropylene aprons, and they wasted 5 rolls of transfer film before they listened. Don’t be that guy.
Third, dimensional stability. This is the big one for R2R, because it’s continuous. If your substrate stretches or shrinks a little as it goes through the machine, the transfer film (which is a separate roll) will get misaligned. One side of the graphic will line up, the other will be off—total garbage. Dimensional stability means the material’s width and length don’t change much when they’re exposed to heat, tension, or humidity. Let’s talk about how this plays out. For example, cotton has terrible dimensional stability—when you heat it and pull tension through the machine, it can stretch up to 5% and then shrink back when it cools. That works for single-piece heat transfer, but for R2R? You’ll get misalignment every time. Polyester, on the other hand, is way more stable—stretches less than 1% under standard tension and heat. Even nylon is okay if you pre-wash it to set the fibers before running through the machine. For non-textiles, PET is stable, polycarbonate is too, but if you’re working with thin polyethylene (PE) film, that’s a problem—it can stretch under the tension of the R2R machine. Pro tip: when you’re ordering substrates, ask the supplier for their “thermal shrinkage rate” and “tensile elongation at break.” If the shrinkage rate is over 2% at your transfer’s temperature, it’s not going to work for continuous R2R runs. I also tell customers to acclimate their substrate rolls to the factory environment for 24 hours before running them—if your factory is super humid, and the substrate came from a dry warehouse, it will absorb moisture and shrink mid-run. That’s a super preventable mistake, but so many people skip it.
Wait, hold on—there are a couple of exceptions, right? Because no rule is 100% perfect. What about if you’re working with a substrate that’s a little tricky, like neoprene or leather? Those have lower heat tolerance than polyester, so you have to run the R2R machine at a lower temperature, slower speed, and use a heat transfer film designed specifically for low-temp substrates. I’ve done test runs with neoprene before where we ran at 320°F instead of 380°F, at 15 feet per minute, and it worked like a charm. What about stretchy materials, like spandex? Same thing—slower speed, lower heat, and make sure the dimensional stability is checked, because spandex stretches a lot. Also, for any substrate that’s porous, like canvas or thick cotton, you have to make sure the transfer ink doesn’t sink too far into the pores. That’s why we recommend using a “hot melt” adhesive transfer for porous materials, instead of a water-based adhesive, which can absorb into the fibers and make the graphic look faded.
Another common question I get: “Can I use the same substrate for R2R and flatbed heat transfer?” Nope, not usually. Flatbed is single-piece, so it can handle a lot more stretch or heat fluctuation because you’re doing it by hand, basically. R2R is automated, continuous, so consistency is everything. A substrate that works for a flatbed might not have enough dimensional stability for a 100-yard roll going through the machine at 40 feet per minute. I had a customer who tried using a flatbed-submitted cotton blend for R2R, and they had to stop every 20 feet to fix misalignment—total disaster.
Now, let’s talk about what happens if you ignore all these rules. I’ve seen it: a customer orders a R2R machine, uses a substrate that’s too oily, runs it at too high a temp, and then blames the machine for being garbage. Half the time, it’s not the machine—it’s the substrate. That’s why before we even sell someone a machine, we do a free 10-minute substrate consultation. We ask them what material they’re using, what kind of graphics they’re transferring, and we point out if their substrate has any red flags. It’s way better than them wasting thousands on rolls of material and transfer film.
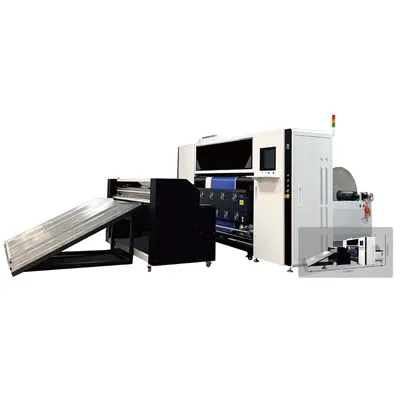
At the end of the day, R2R heat transfer is all about consistency. Your machine is only as good as the material you feed into it. Check the temp tolerance, clean that surface, make sure it doesn’t stretch or shrink mid-run, and test small before you run a whole roll. If you’re still not sure, don’t guess—reach out. I’ve been in this game long enough that I’ve seen every substrate mistake there is, and I can help you avoid them. If you’re ready to chat about your next R2R project, need advice on substrates, or even want to talk about upgrading your machine, just reach out. We’re here to make sure your runs are smooth, your graphics look perfect, and you don’t waste a single roll of material.
Sublimation Printer Wait, one last quick tip: always do a test run with your actual substrate and transfer film before committing to a full production run. Even if you checked all the boxes, there’s always a small variable—like a batch of substrate that’s slightly off. A 10-yard test run takes 10 minutes and saves you from 100 yards of garbage. Trust me, I’ve learned that the hard way.
References
- Hollahan, J. R., & Bell, A. T. (1974). Techniques and Applications of Plasma Chemistry. Wiley-Interscience.
- Horrocks, A. R., & Anand, S. C. (2000). Handbook of Technical Textiles. Woodhead Publishing.
- Shaw, D. J. (1992). Introduction to Colloid and Surface Chemistry. Butterworth-Heinemann.
- ASTM International. (2020). ASTM D4991-20: Standard Test Method for Thermal Shrinkage of Plastic Film and Sheeting.
Hangzhou Yulan Technology Co., Ltd.
Address: Building, No.128 Rihui Road, Linping District, Hangzhou, China.
E-mail: ulinprint@gmail.com
WebSite: https://www.ulinprinter.com/
